
A drawing often specifies hundreds of dimensions, but not every measurement has the same influence on product performance. Some establish appearance. Others determine whether a control panel fits, a seal sits correctly, or a unit fits its intended counter opening. Production control becomes more useful when it reflects those functional relationships.
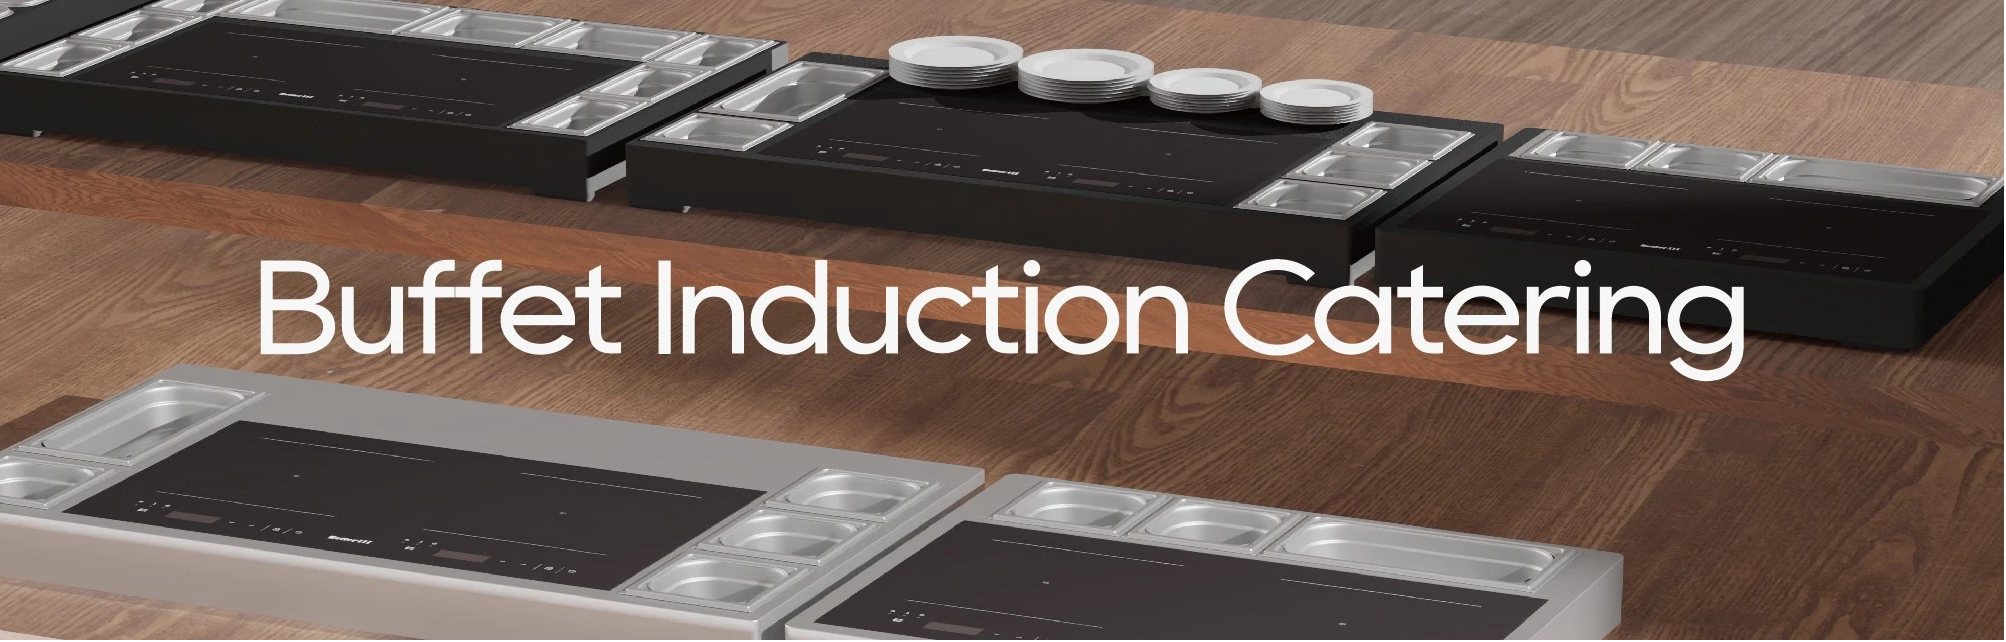
The equipment catalogue of Better Induction includes table-top, drop-in, and integrated induction products. Their different structures illustrate why dimension control begins with assembly functions rather than a generic checklist of every drawing number.
Find Critical Dimensions in Commercial Induction Equipment
Critical dimensions are selected because variation could create a defined problem. The reason for the classification should appear in the engineering record.
Follow interfaces between parts
Start where two parts meet. Relevant interfaces include mounting holes, control openings, wiring routes, fastener locations, seals, and clearances between assemblies. Induction cooker manufacturers define the required relationship, permissible variation, and inspection method.
A stainless enclosure might meet its external dimensions yet still position a control bracket incorrectly. Measuring only overall length and width would not detect that defect. Functional interfaces deserve their own controlled measurement points.
Include installation geometry
Built-in and drop-in commercial induction equipment must fit a specified installation arrangement. Counter opening dimensions, supports, and access to controls and service areas require careful review against the approved model specification.
The BI500F drop-in cooker, for example, has an approximate body size of 40 by 62.5 by 35.3 cm and separate control-box dimensions.
These are overall component dimensions, not validated counter-cutout tolerances or manufacturing datum specifications. The approved production drawing preserves the intended relationships rather than reducing them to one overall size.
Convert Design Intent into Measurable Checks
A drawing tolerance cannot control production unless the inspection method is practical and repeatable. Better Induction and its partners need to define how, where, and when a characteristic is measured.
Choose Measurement Datums for Induction Assemblies
A reference surface or datum establishes how a part is positioned for inspection. Measuring the same feature from inconsistent edges produces different results even when the part has not changed.
Experienced induction cooker manufacturers connect drawing tolerances with manufacturing inspection plans and verified assembly requirements. Better Induction’s integrated development and production capabilities provide relevant context, but the appropriate method still depends on the particular part and assembly.
Set checks at the useful production stage
Some features are best measured before assembly, when the part remains accessible. Others only become meaningful after a bracket, panel, or enclosure has been fitted. The inspection plan reflects those differences.
Measurement frequency follows process risk and observed stability. Repeated measurements also reveal whether fixture positioning or operator technique introduces avoidable variation. Inspecting every minor cosmetic dimension while ignoring a difficult assembly interface wastes effort and provides weak protection against functional defects.
Handle Variation Without Hiding Problems
Production parts vary within controlled limits. The challenge is recognizing when variation threatens the product’s intended fit or operation.
Establish reaction rules for deviations
A control plan identifies the responsible person, containment action, and decision route when a critical dimension falls outside its limit. Operators need to know when to stop using affected parts and how to identify the material produced since the last acceptable check.
A deviation is not normalized simply because assembly workers force components together. Additional pressure or unapproved adjustments might conceal a problem that appears later in use or service.
Link repeated issues to process causes
If measurements show a trend, review fixture condition, tool wear, part positioning, incoming material, or assembly methods. A corrective action should identify the verified cause rather than repeatedly sorting finished parts.
Record before-and-after evidence when a process adjustment is approved. The aim is to control variation at its source and make acceptable assembly predictable across production batches.
Confirm that Measurements Protect the Real Assembly
A dimension control is valuable only when it relates to product function. Periodic review checks whether the chosen measurements remain relevant as designs and production methods change.
Use assembly trials to challenge assumptions
Select parts from representative production variation and verify their fit in the assembled unit.
Check control operation, fastening, access, and other requirements connected with the critical dimensions. An isolated part might pass inspection yet still expose a tolerance-stack problem. Teams document the particular assembly relationships that each trial is designed to challenge.
Trials also help engineers decide whether a tolerance is too restrictive or not restrictive enough. Any revision must follow the normal design-approval process.
Update controls after engineering changes
A new panel, bracket, or control location changes which dimensions matter most. The drawings, fixtures, inspection instructions, and acceptance records are revised together.
Across commercial induction equipment, differences in mounting and workstation layout make this review necessary at model level. Similar induction technology does not imply identical mechanical control points.
Conclusion
Critical dimensions connect directly to fit, access, function, and installation. Induction cooker manufacturers gain more useful controls by measuring the relevant interfaces than by checking every dimension with equal frequency. Identify the important interfaces, define repeatable measurements, and act on deviations before they enter assembly.
Production controls become stronger when they protect the relationships that make the finished equipment work correctly. A measurement datum and reaction rule give every critical tolerance operational meaning. External product dimensions alone cannot establish internal fit limits or an approved installation cutout.
